Introduction
On an automotive interior cutting floor, bad parts rarely show up as a sudden “whole batch scrap” event. More often, they appear as a tuft of loose fibers at the cut edge of a coil mat, a collapsed edge where foam has been pressed inward, a few millimeters of mismatch at a small radius on composite sponge, a clipped corner on a printed logo, a layer of fuzz quietly rising at the edge of a microfiber leather part, and an incomplete cut at the bottom of the fiftieth sheet in a continuous run. Individually, none of these looks dramatic. But when they reach sewing, wrapping, and assembly stations, they turn into rework, trimming, alignment failure, and batch returns. Below, we first clarify the property differences of commonly used automotive interior materials, and then break down six specific process defects—each stuck in material holding, knife-path direction, depth control, or continuous consistency.
1. Common Materials for Automotive Interiors: Know the Material Before You Talk About Cutting
1.1 Leather and Leather-Like Materials: Genuine Leather, Microfiber Leather, PU/PVC Artificial Leather
Genuine leather is a natural fiber structure with grain direction, area-to-area elongation differences, and texture orientation. Microfiber leather looks uniform, but its backing is an ultrafine fiber nonwoven, which is prone to fuzzing and stretching during cutting. PU/PVC artificial leather is a coating plus fabric or foam backing, so cutting must keep the coating from chipping and the backing from unraveling. The common difficulty in this category is not “whether it can be cut,” but the integrity and directional consistency of the cut edge.
1.2 Foams: XPE, EPE, PU Sponge, Composite Sponge
XPE/EPE are closed-cell foams with low density and strong resilience; they compress first and rebound after cutting, so the cut edge easily collapses. PU sponge has an open-cell structure and tends to be “torn” rather than “cut” under lateral force. Composite sponge is a multilayer laminate of sponge plus fabric or leather plus adhesive, so cutting must handle rebound, delamination, and adhesive sticking at the same time. Foam is one of the most knife-path-sensitive material categories in flexible cutting.
1.3 Fiber Felts and Sound Insulation: Needle-Punched Felt, PET Felt, Recycled Textile Felt
These materials are made by needle punching or hot pressing short fibers into felt. They are bulky, prone to edge shedding, and uneven in thickness. During cutting, fibers are easily dragged out by the knife, creating fuzzy trailing edges. In multilayer cutting, inconsistent compression between layers causes dimensional deviation between upper and lower layers. Sound insulation cotton often also has an aluminum foil or coated composite surface, so the knife path must avoid tearing the top layer while still cutting the bottom fibers.
1.4 Coil and Mesh Materials: PVC Coil Mat
A coil mat is neither “cloth” nor “leather”; it is a three-dimensional mesh of interwoven PVC plastic filaments. What is being cut is “a bundle of filaments,” not “a sheet.” After cutting, the coils must not loosen and separate from the cut edge; otherwise, downstream trimming costs more than the cutting itself. This category is extremely heat-sensitive—laser cutting melts and fuses the filaments on contact.
1.5 Composite Laminates: Fabric + Sponge + Adhesive/Film
Automotive seat cushions and soft interior trim extensively use three-layer or more composite structures: a top layer of jacquard fabric or leather, a middle layer of polyurethane sponge, and a bottom layer of adhesive or PE film. Each layer responds differently to cutting—fabric is tough, sponge is resilient, and adhesive film is sticky. The cut quality of a composite laminate is not determined by “the hardest layer to cut,” but by whether all three layers are cut well at the same time without interlayer misalignment.
2. Coil Car Mats: The Problem Is Not “Can’t Cut Through,” but “It Comes Apart After Cutting”
2.1 A Coil Mat Is Not “Cloth”—It Is a Three-Dimensional Interwoven Filament Structure
Magnified, the cross-section of a coil mat is a three-dimensional mesh of PVC filaments intertwined with one another, connected by heat-fused or woven nodes. This means the knife edge is not contacting a continuous plane, but a collection of hundreds of individual filaments. Cutting through is easy, but if the filament ends at the cut edge lose their node constraint, they pull out like the ends of an unraveled rope. The criterion for coil mat cutting quality is not “whether it was cut open,” but “whether the coils at the cut edge are still in place.”
2.2 Three Cutting Methods, Three Ways of Coming Apart: Scissors Loosen Edges, Dies Are Expensive, Lasers Melt Filaments
Manual cutting with scissors or a utility knife produces uneven edges and pulled-out filament ends; loose edges are almost inevitable, and downstream trimming often takes longer than the cutting itself. Die punching gives a neat cut, but every irregular contour requires its own die; a style change means a die change, and the tooling cost of small-batch orders directly eats into profit. Laser hot cutting has a more fundamental problem: high temperature melts and fuses the PVC filaments, making the cut edge hard, lumpy, and harsh to the touch, while also generating irritating chlorine-containing smoke. For export orders, environmental testing and odor rating are hurdles it simply cannot pass.
2.3 ZINGCUT’s Approach: Cold Cutting Preserves Filament Shape, Vision Cuts Along the Pattern
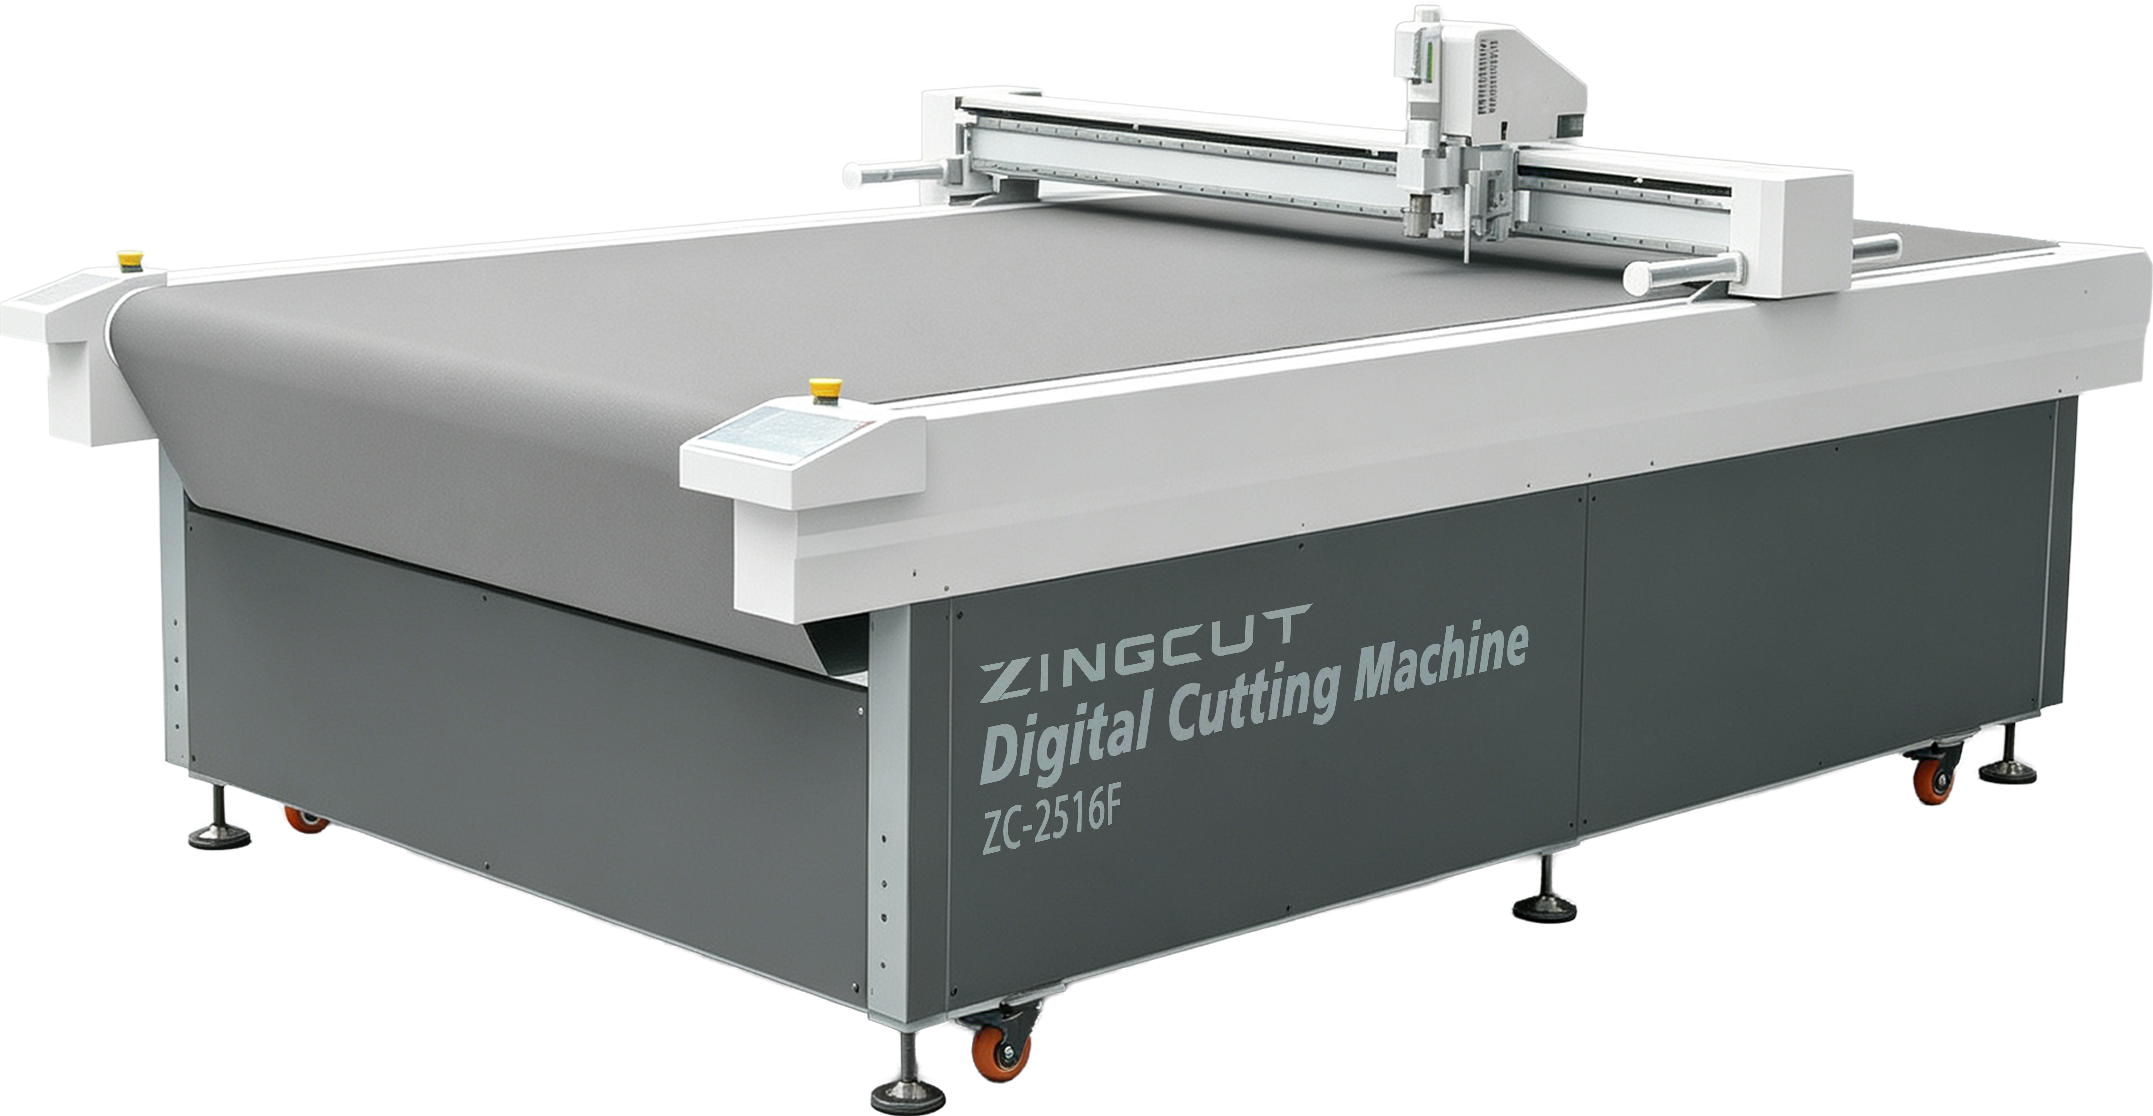
ZINGCUT’s configuration logic for coil mats targets the two scrap sources—“loose filaments” and “melted filaments.” The high-frequency oscillating knife cuts the coil mat by physical cold cutting, with no heat source involved, so filament ends are neither fused nor stuck together, and the cut edge retains its original elastic feel. CCD vision positioning solves the alignment problem for printed logo or pattern-contour coil mats—the knife path follows the actual pattern on the material instead of forcing a CAD file onto it. The difficulty of coil mats has never been “whether it can be cut,” but “after cutting, the coils are still coils—not a pile of loose plastic fuzz.”
3. XPE/EPE Closed-Cell Foam: By the Time the Knife Goes Down, the Material Has Already Been “Crushed”
3.1 The “Compress First, Cut Later” Dilemma of Closed-Cell Foam
The mechanical behavior of XPE and EPE closed-cell foams has a key feature: before the knife edge actually penetrates, the material is first elastically compressed by the pressure applied by the knife body. After the knife leaves, the material rebounds, and the cut edge is not vertical but slightly concave—a collapsed edge. Low-density EPE is even more obvious—before the knife cuts through, the material has already been flattened around the cut. This means dimensional deviation in foam cutting is often not “cut off the line,” but “deformed before cutting.”
3.2 Band Saw Side Squeeze, Die Overall Compression, Hand Knife Drag—Three Forms of Edge Collapse
Band saw cutting squeezes the foam laterally with the blade, collapsing one side of the cut and tearing the other, especially in thick material. Die punching applies overall downward compression; the foam is compressed inside the die cavity and then rebounds, so the cut size is one size smaller than the die, with small radii and narrow slots suffering most. Hand knife drag cutting introduces lateral pulling force, and low-density foam is directly “torn open” rather than cut, leaving a rough edge and unpredictable dimensions. The three methods produce different scrap forms, but the root cause is the same: the material is subjected to forces it should not experience during cutting.
3.3 The Principle Advantage of Oscillating Knives—and Why Ordinary Oscillating Knives Still “Sweep” Material
Oscillating knives avoid the compression problem because the blade vibrates at high frequency and “pecks” into the material; the dwell time is extremely short, and the foam is separated before it has time to compress. But this does not mean every oscillating knife can cut foam well. When an ordinary straight blade travels quickly along a curve, the blade body exerts a lateral “sweeping” force on the material, causing overcut or undercut at corners, and edge collapse migrates from straight sections to curved sections. If the knife head’s vibration direction is not strictly constrained to the vertical direction, the scrap rate on curved cuts rises noticeably.
3.4 ZINGCUT’s Control Logic: Vertical Vibration Constraint + No Material Sweeping on Curves
ZINGCUT’s control point on closed-cell foam is not simply increasing vibration frequency, but strictly constraining the vibration direction to vertical so that the blade body does not “sweep” the material when cutting curves. The cut-edge verticality at corners stays consistent with straight sections. For step edges, locating holes, and irregular contours on XPE car mats, cut-edge verticality matters more than peak speed in determining whether the finished part can go directly to assembly. Foam scrap is often not “not cut through,” but “not cut square.”
4. Composite Sponge Seat Cushions: “Adhesive Sticking to the Knife” and “Rebound After Cutting” Are Two Different Problems
4.1 The Three-Layer Structure of Composite Sponge: Fabric/Leather + Sponge + Adhesive
The typical cross-section of composite sponge for automotive seat cushions has three layers: a top layer of jacquard fabric or perforated leather, a middle layer of polyurethane sponge (density from 25D to 60D), and a bottom layer of adhesive or PE film. The three layers respond completely differently to cutting—the fabric layer needs a sharp cut without unraveling, the sponge layer needs low lateral force without edge collapse, and the adhesive layer needs anti-sticking. Any single cut through all three layers must satisfy three sets of material properties at the same time.
4.2 Rebound Dimensional Deviation: Why Small Radii and Narrow Slots Do Not Match
Sponge is compressed when the knife presses down, and after cutting it rebounds, so the actual size does not match the drawing. Low-density sponge collapses under pressure and “shrinks back” after cutting; high-density resilient sponge has a large elastic recovery, and deviation is most obvious at narrow slots and R corners. The insidious part of this problem is that straight sections and large contours look fine, while scrap concentrates at small radii, narrow strips, and locating holes—exactly the features that sewing stations rely on most for alignment.
4.3 Adhesive Sticking to the Knife: The Cut Edge Suddenly Turns Fuzzy from a Certain Cut Onward
The bottom adhesive or adhesive film sticks to the blade after being heated or pressed during cutting. The knife becomes progressively “duller,” and the cut edge suddenly turns fuzzy from a certain cut onward. Operators often discover the problem only at final inspection, but scrap has already been accumulating since that cut. Adhesive sticking is especially prominent in hot summer workshops and with low-melting-point adhesive films. Simply increasing knife speed does not solve it; it may even worsen adhesion by increasing friction heat.
4.4 ZINGCUT’s Layer-by-Layer Depth Control and Zoned Vacuum Adsorption
ZINGCUT’s approach in composite sponge is not “one knife setting for everything,” but matching cutting parameters to each material layer: Z-axis depth control sets the penetration depth by layer, and the adhesive layer uses a matched blade type and vibration frequency to reduce sticking. Zoned vacuum adsorption adjusts pressure by sponge density—too much negative pressure in low-density areas deforms the sponge, while insufficient holding force in high-density areas causes sliding. For composite sponge seat cushion parts, dimensional tolerance and edge fuzz may not appear on the same inspection sheet, but at the sewing station they are the same problem.
5. Printed Fabrics and Logo Car Mats: If the Knife Path Does Not Match the Pattern, the Whole Batch Is Scrap
5.1 Pattern Position on Printed Material ≠ Theoretical CAD Position
Printed fabrics undergo slight deformation, offset, and stretching during printing, winding, and spreading. The pattern position in a CAD file is a theoretical value; the actual pattern position on the material is something else. The deviation may be only a few millimeters, but for logo contour cutting and registered parts, a few millimeters is the difference between uneven margins and a clipped pattern corner. No matter how high the pure geometric accuracy of the equipment, if the knife path only trusts the file and not the material, this deviation is destined to exist.
5.2 Scrap Forms: Uneven Margins, Clipped Pattern Corners, Batch-Wide Alignment Failure
Scrap in printed interior parts is not “cut badly,” but “cut off-register”—the cut itself is smooth and neat, but its position relative to the pattern is wrong. A brand logo on a coil mat with one corner clipped, a jacquard seat cover pattern contour with a wide margin on one side and a narrow margin on the other, a registered part with the pattern extending beyond the part edge—these are typical scrap forms caused by the absence of vision alignment. Such defects are easily missed in spot checks and only surface in concentrated form at assembly or customer acceptance.
5.3 ZINGCUT’s CCD Vision Alignment: The Knife Follows the Pattern
ZINGCUT’s configuration logic for printed interior parts is straightforward: CCD vision first identifies the actual pattern position and angle on the material, then generates the knife path, instead of forcing a theoretical file onto the material. For coil mat logo contours and printed leather registered parts, the knife follows the pattern, not the other way around. For factories running both plain materials and printed materials, the vision module is not mandatory on every machine—but once printed orders are accepted without vision, the scrap rate is not a matter of “being slightly high”; it is batch-wide.
6. Microfiber and Genuine Leather Interior Surfaces: “Backing Pull” and “Grain-Direction Color Difference” Are Hidden Scrap
6.1 The Hidden Defect of Microfiber: Backing Pull and Edge Fuzzing
Microfiber leather looks uniform, but its backing is an ultrafine fiber nonwoven structure. If the material is not securely held or the knife path direction is wrong during cutting, backing fibers are dragged out by the knife, causing edge fuzzing and local deformation. In a stack of cut parts, such scrap looks “dimensionally correct,” but at the wrapping or sewing station, exposed fuzz and thickened edges directly downgrade the finished appearance. Microfiber cutting quality is not only about cut-edge neatness; it is about whether backing fibers have been pulled out.
6.2 Multilayer Spreading Slippage: Curvature Misalignment Only Shows Up at the Wrapping Station
Microfiber roll material has low surface friction, and when multiple layers are spread and cut, upper and lower layers tend to micro-slip. A single cut part may measure fine when picked up, but parts of the same pattern from different layers are misaligned in curvature and fail to match at the wrapping and splicing station. Slippage is most obvious during fast curve travel and corner reversals; the root cause is insufficient adsorption force in local areas or incomplete interlayer contact during spreading.
6.3 Genuine Leather Grain Direction: Dimensions Are Right, but Color Difference Appears
Genuine leather is a natural material with grain direction, area-to-area elongation differences, and texture orientation. If the grain direction of a cut part does not match the pattern requirement, the sewn seat cover shows color difference under light, even though the cutting inspection says the dimensions are fully qualified. At curves and sharp corners, if the knife path does not follow the fiber direction, pull-induced notching can occur, leaving a rough edge that requires manual trimming. Half of genuine leather cutting scrap is not on the dimensional sheet—it is in direction and grain.
6.4 ZINGCUT’s Adsorption Stability and Knife-Path Direction Constraints
ZINGCUT’s control point on surface materials is not “cut faster,” but “the material is stable before cutting, and the knife path is correct during cutting.” Zoned vacuum holds microfiber roll material and multilayer stacks flat, reducing micro-slip during feeding and cutting. At the knife-path level, pattern grain-direction requirements and curve cutting direction are incorporated into nesting constraints, rather than sorted out manually after cutting. Microfiber and genuine leather scrap is often determined before the knife goes down—by spreading and direction.
7. Consistency Decay in Continuous Production: The First Sheet Looks Great, the Fiftieth Starts Missing Cuts
7.1 First Test Cut Looks Great, the Fiftieth Sheet Misses Cuts—Adsorption Decay Is the Main Cause
Oscillating knife cutting relies on vacuum adsorption to hold material on the table. With new equipment, new sealing strips, and sufficient suction, the first test cut has a beautiful edge and clean unloading. But after dozens of sheets in continuous operation, table sealing strips age locally and edge areas leak air. The material bulges slightly during cutting, the actual knife depth is insufficient, the bottom is not cut through, and the part tears out with a fuzzy edge during unloading. Operators may not immediately connect the scrap to “suction,” because the upper part of the cut edge looks fine.
7.2 Table Sealing Strip Aging and Uneven Zoned Suction
Vacuum adsorption on a large-format cutting table is zone-controlled, but the sealing strips and pipe joints between zones age gradually. Edge areas and areas where small parts are placed are often the first to lose suction, while the central area covered by large parts still holds well, creating the illusion that “large parts are fine, small parts keep missing cuts.” Uneven zoned suction also causes inconsistent cutting depth at different positions on the same sheet, making scrap distribution irregular and troubleshooting difficult.
7.3 Progressive Blade Dulling: From “Cutting” to “Squeezing”
Blade wear is a gradual process. After the blade tip dulls, the actual cutting depth becomes shallower, and the cut changes from “cutting” to “squeezing.” Edge collapse in foam and sponge quietly returns, and microfiber fuzz reappears. Dulling does not trigger an alarm; it only makes the scrap rate climb slowly. Operators who judge blade-change timing by feel are often late; by the time the cut edge is visibly fuzzy, a batch of borderline scrap has already accumulated.