Introduction
If you are looking to purchase a CNC cutting machine for your shoe factory, the market is flooded with choices. But do all “CNC leather cutters” or “fabric cutters” truly understand the unique demands of footwear manufacturing?
From highly elastic flyknit uppers to thick, shock-absorbing EVA soles, and from ultra-thin insoles lacking rigidity to precise side panels requiring strict tolerance—every shoe component presents a different challenge. The wrong machine will not only fail to improve your yield rate but will also increase your die costs and material waste.
1. What are the most common pitfalls in flexible cutting for footwear?
1.1 Why is cutting flyknit and mesh uppers much harder than many buyers expect?
Upper materials have strong elasticity, almost like socks. Traditional clamping bars only hold the edges, while the suspended middle section shifts the moment the blade goes down, leading to frayed edges, burrs, or even dimensional distortion. To maintain yield rates, factories often have to slow down and cut fewer layers, which directly bottlenecks production capacity.
1.2 Before asking for a machine price, what should I check first?
For shoe factories, buyers usually need to handle small, irregular components and cope with frequent style changes. Before clarifying these basic questions, I never look at the quote: Material and thickness determine the tool selection; Maximum cut piece size determines the table size; Daily output target determines the cutting speed and workflow; Whether punching or marking is needed determines the tool module expansion; and Order type determines the quality of the nesting software. I don’t trust any low price before these questions are answered. The wrong machine often fails in the details: it might cut, but the edges will be full of burrs. They might all look similar, but once on the assembly line, the daily yield gap becomes immediately obvious.
2. Which tool configuration is the most practical for cutting footwear materials?
2.1 For flyknit and mesh uppers, why do traditional die-cutting and standard blades fail?
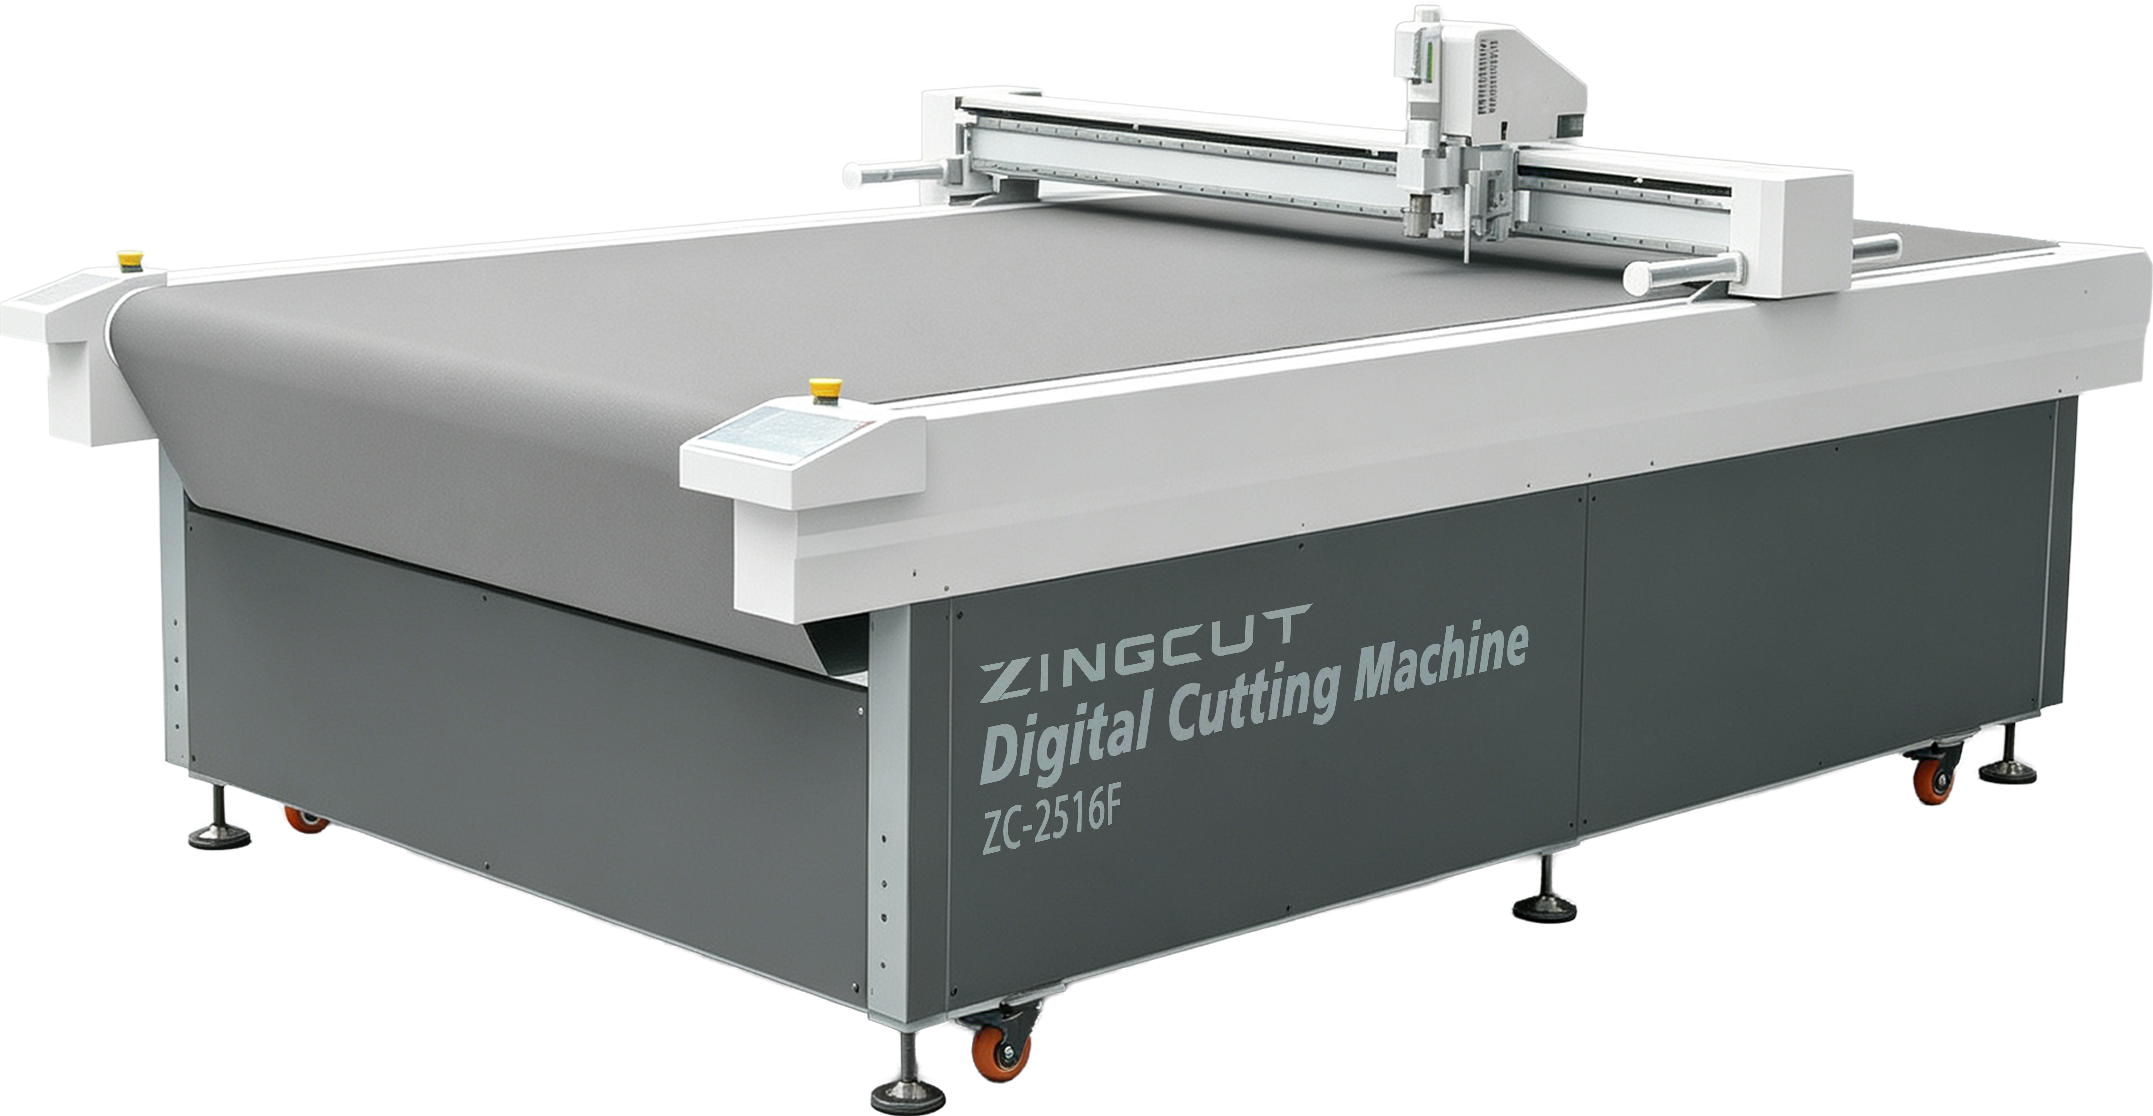
Many factories think they can just put a blade on a machine and cut uppers—this is a huge misconception. When a standard blade cuts into flyknit or mesh, it creates a dragging force that directly damages the material structure and causes fraying. This absolutely requires high-frequency oscillating cutting technology (vibrating knife)—the blade micro-moves up and down tens of thousands of times per minute, cutting the material like an ultra-fine saw. This guarantees perfectly flat, non-burnt edges. Meanwhile, it supports direct CAD file imports, completely eliminating the cost of making dies and the 3 to 5 days of waiting time. In this regard, ZINGCUT’s high-frequency oscillating tool heads are specially adapted for these materials, specifically to help shoe factories take on those small-batch, fast-turnaround urgent orders.
2.2 Why do footwear components need a “dash” or “small U” notch cut on the edge after cutting?
When buying a machine, don’t just look at whether it cuts the outer contour straight; look at whether it can handle the work of downstream processes along the way. Pure visual alignment for upper splicing easily leads to misalignment. If the machine can simultaneously cut a “dash” or “small U” notch for registration during cutting, sewing workers can simply match “notch to notch” to sew, instantly doubling efficiency. ZINGCUT’s multi-tool carriage supports synchronous cutting and precise notching in a single pass, eliminating secondary operations and truly saving labor for the factory.
2.3 What should I pay attention to in tool configuration when cutting thin insoles?
Insoles lack their own rigidity and rely entirely on external fixation. The material easily yields or rolls up the moment the blade touches it. The vibration frequency must be stable, and it needs to be paired with a specialized vacuum film to cut smooth, burr-free curves for the arch and heel.
3. Why is the vacuum hold-down system so important?
3.1 Why do I recommend that upper cutting must be equipped with multi-zone vacuum suction?
Elastic fabrics and mesh easily shift during cutting. Zoned vacuum can freeze the entire roll of fabric onto the table. It’s not about having more zones, but being able to independently control suction based on the nesting layout—only when the material stays still does precision have any meaning.
3.2 During continuous feeding of rolled uppers, how do you ensure the material doesn't shift?
This is the key to doubling production capacity and is the ultimate test of the machine’s underlying design. Continuous feeding means the machine is moving material without stopping, while the cutting area must maintain extremely high suction. If the conveyor belt permeability is too high or the fan negative pressure is insufficient, the material will wrinkle or deviate during dynamic transport, and the blade will ruin it upon contact. You must rely on a high-torque automatic feeding system combined with a high-power variable frequency fan to establish a strong sealed negative pressure the moment the material enters the cutting zone.
3.3 What else affects the hold-down force for thin materials?
Besides the suction power, whether the table surface is flat is crucial. Once the table has dents or deformation, it will severely leak air, making it impossible to suction locally. In addition, the permeability of the table felt, film covering techniques, and even the workshop’s temperature and humidity will affect how ultra-thin materials (like insole lining) adhere at the exact moment of cut separation.
4. Why does the machine frame transmission determine splicing precision?
4.1 In what aspects will buyers most clearly feel the difference in frame rigidity?
Many machine quotes only list the working size and motor power, hiding the transmission system in a corner. But it’s precisely this difference that is felt most deeply in real factory scenarios:
· When cutting large patterns or long strips (like genuine leather): Long-distance movement requires extremely stable motion; otherwise, the cut lines will be wavy.
· When facing higher daily output: The machine runs for over ten hours a day with repeated rapid stops and starts; if the transmission system isn’t durable, it will cause frequent downtime.
· When integrating with a continuous feeding line: Continuous operation requires strong power transmission, otherwise, it can’t pull the rolled materials.
In summary, these scenarios test not just speed, but whether accuracy can remain absolutely stable from end to end.
4.2 What about the crossbeam strength and structure?
This involves the machine’s “skeleton.” I pay extreme attention to the crossbeam structure because it directly determines motion stability and cutting response. If the beam is too weak, it will visibly oscillate during rapid cutting or when cutting harder shoe materials. This tiny vibration directly affects the blade quality and cutting positioning accuracy. Buyers must ask: What is your beam structure? What is the wall thickness? What is the assembly precision?