Introduction
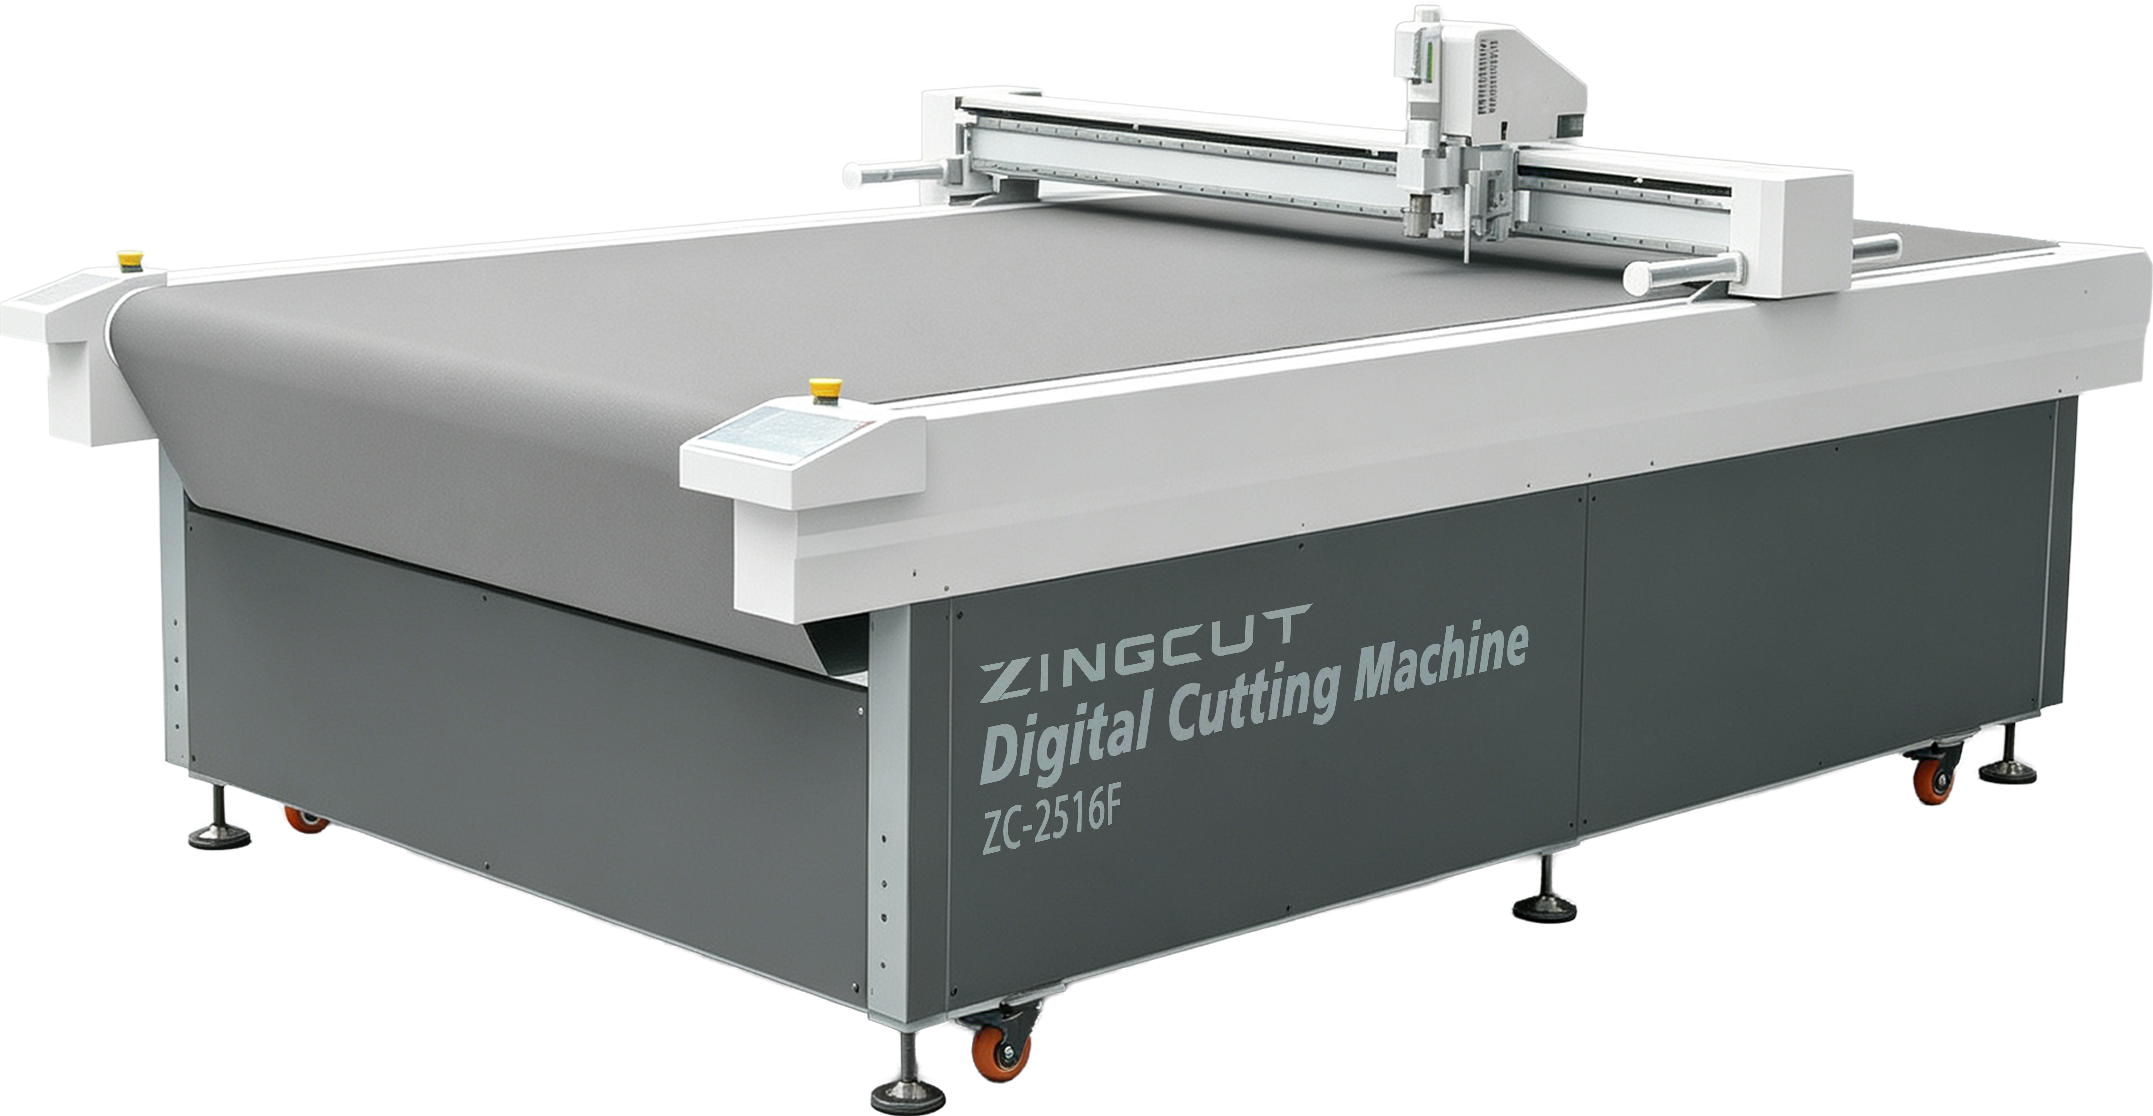
Many manufacturers evaluate a cnc cutting machine solely by its cutting performance, while overlooking the fact that a carton still has to go through creasing, folding, and forming. Cutting defines the outline, creasing defines the fold lines, and material thickness and machine condition in turn affect accuracy. If a cnc cutting machine is treated only as a sheet-cutting device, even excellent cutting can be offset by skewed fold angles, score-line cracking, or flaps that will not close properly.
1. Why Good Cutting Performance Does Not Equal a Good Carton
Cutting produces a two-dimensional outline, but the “quality” of a carton is defined only after three-dimensional forming. No matter how high the outline accuracy is, if any one of thickness, cut edge, or creasing is out of control, the squareness of the finished carton will deteriorate.
1.1 What Factors Affect Carton Accuracy ?
· Thickness: Thickness changes the dimensional reference. The position of die-cut creases will deviate with board thickness, especially after laminated corrugated board is used; thicker boards also have a narrower tolerance window for creasing depth.
· Cut edge: The cut edge is not just about whether there are burrs. Crushed flutes or micro-cracks in the liner can extend from the cut edge toward the crease line during folding, creating a hidden source of score-line cracking.
· Creasing: Creasing is most directly related to forming. If it is too shallow, the board will spring back after folding and the fold line will drift; if it is too deep, the liner fibers will be cut, and the fold angle will show whitening or even break.
1.2 Cutting Requirements for Common Packaging Materials
Different packaging materials vary greatly in structure and thickness, so the same cutting and creasing parameters cannot be applied to all of them. The table below lists the main risks and process priorities for common materials.
| Material | Structure and Thickness Characteristics | Main Cutting/Creasing Risks | Process Priorities |
|---|---|---|---|
| Thin corrugated (E-flute, approx. 1.1–1.6 mm) | Low flute height, fine liner | Creasing too deep causes score-line cracking; excessive cutting pressure crushes the flute | Low pressure, short-stroke oscillating knife; creasing depth 0.5–0.7× total thickness |
| Single B-flute (approx. 2.5–3.0 mm) | Balanced cushioning and stiffness, most commonly used | Insufficient crease width causes “fish tailing” after folding; unclean cuts make fold angles weak | Crease width 1.2–1.5× board thickness; pay attention to slotting-to-crease registration |
| BC double-wall (approx. 6–7 mm) | Thick, rigid, mainstay for outer boxes | Creasing must actually crush the corrugated layer, otherwise severe springback; cutting too fast leaves the bottom uncut | Reduce cutting speed; use three-piece creasing wheels rather than single-piece hard pressing |
| Honeycomb board | Hollow-core structure, thickness can reach tens of millimeters | Excessive knife pressure directly crushes cells; vacuum adsorption may also deform the honeycomb structure | Controlled-depth oscillating cutting; extremely sharp blade to reduce downward pressure |
2. Cutting Is the Foundation for Making a Good Carton
Cutting is the “foundation” not because it alone can make a good carton, but because it sets the error limit for all subsequent processes.
2.1 Impact of Cutting Accuracy on Cartons
Carton folding is based on the cut outline. If the outline dimensions deviate, the crease lines—even if accurate in themselves—will be installed at the wrong coordinates. Cutting accuracy can usually reach the ±0.1 mm level, but if the material slips or vacuum adsorption is uneven, the actual knife position will deviate from the programmed path, and subsequent creasing and folding will lose a reliable reference. For box types requiring precise registration, this deviation will be amplified by folding into visible seam misalignment.
2.2 Impact of a Clean, Sharp Cut Edge on Cartons
A clean, sharp cut edge means cutting occurs at the fiber level rather than by tearing or crushing. High-frequency oscillating cutting relies on a short stroke and high frequency to separate the material locally and rapidly, rather than by brute downward force. Once burrs or crushed flutes appear at the cut edge, folding stress will concentrate and release from these microscopic defects, making the outer liner at the fold angle more prone to cracking. The role of cutting quality here is to “avoid creating weak points.
3. How Thickness Affects Cutting Accuracy
3.1 Differences in Cutting Processes Between Thin Board and Thick Corrugated Board
Thin board (E-flute and below): The main risk is over-processing. A slightly dull blade or excessive pressure can crush the weak flute structure while the cut still “looks complete.” Use short-stroke, high-frequency oscillation with low downward pressure.
· Thick corrugated board: The knife must stay sharp across a greater thickness, otherwise the bottom is uncut or torn. Chip removal and heat dissipation are worse, so cutting speed should be reduced. Honeycomb board is even more fragile and requires controlled cutting depth and stable bottom support to avoid crushing the cells.
3.2 Why 0.5 mm Thickness Is the Best
A clarification is needed: “0.5 mm” does not mean that 0.5 mm is the optimal thickness of the board itself; it refers to the process window of creasing depth relative to the total corrugated thickness. Practice shows that when the creasing depth is 0.5–0.7× the total thickness, the board can form a stable plastic hinge without cutting the liner fibers. Below this window, the crease is too shallow and springback after folding occurs; above this window, the liner enters the fracture zone and the risk of score-line cracking rises. What is truly “best” is not a fixed material thickness, but the ability of the cutting and creasing system to stably control the creasing depth at around 0.5× the total thickness.
4. The Importance of Creasing
4.1 What Are Creasing and Crease Lines?
Creasing is not simply “pressing a line into the board.” Its mechanical purpose is to create a controlled plastic hinge: the creasing wheel causes local yielding along a predetermined line so folding force is concentrated there. Crease width and depth define the hinge’s tightness—too narrow raises stress concentration and cracking risk; too wide over-crushes the flute and weakens fold stiffness.
4.2 Creasing Determines Whether the Folding Path Is Straight and Whether the Carton Is Square
Folding follows the path of least resistance. If crease depth, width, or position varies, the board bends within the crease band instead of along the designed axis, causing twisted panels and “fish tailing”—misaligned flaps and lost squareness. Squareness is largely set at creasing, not corrected later by the folding machine.
4.3 Why Common Creasing Defects Occur
Common creasing defects do not occur randomly; they have a clear causal chain:
· Crease too shallow / insufficient line width: springback after folding, fold-line drift, flaps that do not close properly.
· Crease too deep: liner fibers are cut, causing score-line cracking and whitening at the fold angle.
· Crease direction does not match flute direction: when creasing perpendicular to the flutes, the corrugated layer is crushed as a whole, and the fold angle is weak and prone to breaking.
· Improper board moisture content: below 7%, fibers become brittle and creasing will crack; the reasonable range is 8%–12%.
· Slotting knife wear or registration deviation: rough slot edges, or a 1–2 mm misalignment between crease line and slot, will be exposed in the form of “flaring.”
4.4 How We Solve These Problems
| Defect/Risk | Main Cause | Solution |
|---|---|---|
| Springback after folding, fold-line drift | Crease too shallow or insufficient line width | Lock creasing depth at 0.5–0.7× total corrugated thickness; line width 1.2–1.5× board thickness |
| Score-line cracking, whitening | Crease too deep, liner fibers cut | Control the upper limit of creasing depth; avoid single-piece hard disc pressing; use a combination of upper convex wheel, lower groove, and elastic pad |
| Weak or easily broken fold angle | Crease direction does not match flute direction | Optimize box layout and crease direction; adjust flute direction when necessary |
| Creasing cracks | Board moisture content below 7% | Confirm moisture content is 8%–12% before cutting; do not compromise by “creasing shallower” for dry board |
| Rough slots, crease misalignment | Slotting knife wear or registration deviation | Regularly inspect slotting knives and registration; complete cutting and creasing in the same coordinate system to ensure repeatable registration |
5. The Machine Is Not Independent: Equipment Condition and Operating Parameters Are Equally Critical
No matter how high the factory accuracy of a machine is, its actual output accuracy is determined by the weakest link among knife condition, calibration status, and parameter settings.
5.1 Knife Wear, Equipment Calibration, and Daily Maintenance
· Knife wear: A worn edge first loses its ability to “separate cleanly.” When the operator increases downward pressure to cut through, this pressure also crushes the material on both sides of the cut, causing flute crushing and dimensional deviation.
· Equipment calibration: After each knife change, recalibrate the Z-axis or knife height to ensure accurate cutting depth; thermal expansion and accumulated vibration will gradually shift the cutting head, so calibration and alignment status should be checked regularly.
· Daily maintenance: Vacuum adsorption uniformity also falls under calibration. Uneven adsorption can cause slight material displacement during cutting, making outline accuracy impossible to guarantee.
5.2 Cutting Pressure, Speed, and Parameters
Parameters are interdependent. Higher speed without a sharp edge leaves the bottom uncut; more pressure without checking sharpness crushes flutes. Use a sharp knife, the lowest pressure that cuts cleanly, and speed matched to thickness and density. Thin materials: short stroke, high frequency. Thick materials: lower speed for consistent cut quality. Fine-tune per batch.
5.3 Simplified Operation to Reduce Production Incidents Caused by Operator Experience
Staff turnover and frequent order changes make “operator feel” unreliable. The fix is not a simpler interface but repeatable calibration, knife setting, and parameter selection, so every shift uses the same validated configuration instead of trial-cutting from scratch. Standardizing knife-height calibration, vacuum-zone selection, and cutting-depth settings reduces batch deviations from human judgment.
6. How Zingcut Helps You Improve Production Efficiency While Making Good Cartons
Cutting quality and production efficiency are not inherently opposed. What truly creates conflict between them is often “non-cutting” links such as material handling, tabletop cleanliness, and equipment availability. Zingcut can provide related accessories for you to purchase as optional add-ons, addressing these links to improve overall efficiency.
6.1 Is Heavy Material Also Quietly Slowing Down Production Efficiency?
Manual handling of large-format board is slow and inconsistent, causing repeated knife setting and first-piece scrap. Zingcut offers an optional material lifter for purchase, keeping feed height aligned with the cutting table, reducing placement deviation, and stabilizing adsorption, knife setting, and continuous production.。
6.2 Are the Chips Left After Cutting Often Difficult to Clean Up?
Paper dust and chips can enter guide rails, the knife area, and the vacuum system, increasing wear, disrupting adsorption, dulling blades, and causing cleaning downtime. Zingcut offers an optional tabletop dust collector for purchase to capture dust at the source, protect the table, rails, and adsorption system, and reduce unplanned interruptions.